
Latest Products
Contact Us
- No.5 Industrial Road Panjia Industrial Zone. Xueyan Town, Wujin District, Changzhou City,Jiangsu Province China.
- mary@cnhengjiu.com
- xmt@cnhengjiu.com
- dyy@cnhengjiu.com
- +86-519-86541389

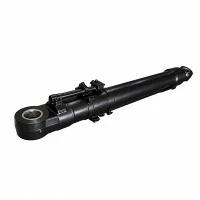
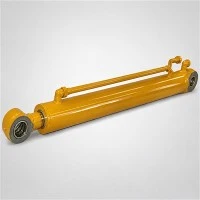
Rapid Forging Press Side Cylinder
Rapid Forging Press Side Cylinder represent a pinnacle in the production of high-precision, seamless hydraulic cylinders. This two-stage cold-working process transforms a rough, honed, or extruded steel tube into a component with exceptional surface characteristics and dimensional accuracy, making it ideal for demanding hydraulic and pneumatic applications.
Description
Jiangsu Ying Naisi Machinery Manufacturing Co., Ltd. is one of the leading manufacturers and suppliers of Rapid Forging Press Side Cylinder in China. We are committed to providing high quality customized service and OEM&ODM service for global clients. If you're going to wholesale advanced Rapid Forging Press Side Cylinder made in China, welcome to get quotation from our factory. For price consultation, contact us.
Rapid Forging Press Side Cylinder represent a pinnacle in the production of high-precision, seamless hydraulic cylinders. This two-stage cold-working process transforms a rough, honed, or extruded steel tube into a component with exceptional surface characteristics and dimensional accuracy, making it ideal for demanding hydraulic and pneumatic applications.
The process begins with skiving. In this first stage, a single-point cutting tool is passed through the bore of the tube. Its primary function is to remove a controlled layer of material from the internal surface. This achieves two critical objectives: it eliminates surface imperfections and inconsistencies from the base material, and it establishes the exact final inner diameter with extremely tight dimensional tolerances. Skiving effectively prepares a perfectly uniform canvas for the next crucial step.

The second stage is roller burnishing. This is a chipless finishing process where hardened, precision rollers are forced under high pressure against the skived inner surface. The rollers cold-work the metal, compressing the peaks of the microscopic surface profile into the valleys. This plastic deformation yields a multitude of benefits:
The combination of these processes results in a tube that offers unmatched performance. The skiving ensures perfect geometry and size, while the roller burnishing optimizes the surface integrity. Consequently, these tubes are the preferred choice for hydraulic cylinders in heavy machinery, industrial equipment, and mobile applications where reliability, efficiency, and longevity are paramount. Their seamless nature and superb finish contribute to lower operating costs through reduced friction, minimized leakage, and decreased downtime.
1. Chemical Composition
|
Steel grade |
Chemical composition % |
||||||||
|
C |
Si |
Mn |
P |
S |
Cr |
Ni |
V |
AI |
|
|
≤ |
≥ |
||||||||
|
C20 |
0.17-0.24 |
0.17-0.37 |
0.15-0.65 |
0.035 |
0.025 |
0.250 |
0.250 |
/ |
/ |
|
CK45 |
0.42-0.5 |
0.17-0.37 |
0.5-0.8 |
0.025 |
0.025 |
0.250 |
0.300 |
/ |
/ |
|
Q355B |
≤0.2 |
≤0.5 |
1.0-1.6 |
0.030 |
0.030 |
0.030 |
0.250 |
0.080 |
0.015 |
|
Q355D |
≤0.2 |
≤0.5 |
1.0-1.6 |
0.030 |
0.025 |
0.250 |
0.250 |
0.150 |
/ |
|
E355(ST52) |
≤0.22 |
≤0.55 |
≤1.6 |
0.025 |
0.025 |
0.250 |
0.250 |
/ |
/ |
|
SAE1026 |
0.22-0.28 |
0.15-0.35 |
0.6-0.9 |
0.040 |
0.050 |
/ |
/ |
/ |
/ |
|
4130 |
0.28-0.33 |
0.15-0.35 |
0.4-0.6 |
0.040 |
0.040 |
0.80-1.10 |
/ |
/ |
/ |
|
4140 |
0.36-0.43 |
0.15-0.35 |
0.705-1.0 |
0.040 |
0.040 |
0.80-1.10 |
/ |
/ |
/ |
2.Mechanical Property:
|
Delivery condition |
Cold finished(hard)(BK) |
Cold drawn and stress-relieved(BK+S) |
|||
|
Steel grade |
Rm MPa |
Elongation A5% |
Rm MPa |
ReH Mpa |
Elongation A5% |
|
C20 |
≥550 |
≥5 |
≥520 |
≥375 |
≥15 |
|
CK45 |
≥645 |
≥5 |
≥600 |
≥520 |
≥10 |
|
Q355B |
≥640 |
≥5 |
≥600 |
≥520 |
≥14 |
|
Q355D |
≥640 |
≥5 |
≥600 |
≥520 |
≥14 |
|
E355(ST52) |
≥640 |
≥5 |
≥600 |
≥520 |
≥14 |
|
SAE1026 |
≥640 |
≥5 |
≥600 |
≥520 |
≥15 |
3.Tolerance:
|
Tolerance |
I.D Tolerance |
Tolerance of wall thickness |
||||
| Size of I.D. | H8 | H9 | H10 |
<120mm(O.D) ≥120mm up to 210mm >210mm |
±5% ±7.5% ±10% |
|
|
30 |
0.033 |
0.052 |
0.084 |
|||
|
>30-50 |
0.039 |
0.062 |
0.1 |
|||
|
>50-80 |
0.046 |
0.074 |
0.12 |
|||
|
>80-120 |
0.054 |
0.087 |
0.14 |
|||
|
>120-180 |
0.063 |
0.1 |
0.16 |
|||
|
>180-250 |
0.072 |
0.115 |
0.185 |
|||
|
>250-315 |
0.081 |
0.13 |
0.21 |
|||
|
>315-400 |
0.089 |
0.14 |
0.23 |
|||
4.Processing Form
|
Processing form |
I.Dmm |
Length |
Straightness |
I.D tolerance |
I.D Roughness (RA) |
|
Honed |
40-500 |
≤12M |
0.5-1/1000 |
H8-H9 |
0.4-0.8um |
|
SRB |
50-250 |
≤12M |
0.5-1/1000 |
H8 |
0.1-0.4um |
Hot Tags: Rapid Forging Press Side Cylinder, China Rapid Forging Press Side Cylinder manufacturers, suppliers, factory, Skived And Roller Burnished Tubes, hydraulic honed tubes, st52 din2391 seamless pipe shock absorber honed, Honed Tubes For Hydraulic Cylinders, Stainless Steel Honed Tube, Precision Cold Drawn Honed Steel Tubing
You Might Also Like


